TAAT e-catalog
for
Development partners
https://e-catalogs.taat-africa.org/org/technologies/mechanized-defeathering-and-egg-sorting
Efficiency Unleashed: Poultry Processing, Simplified
Mechanized defeathering and egg sorting technology revolutionizes poultry processing by streamlining two critical aspects of the production process. These machines complete the feather removal process in just 30 seconds. Moreover, removed feathers are collected through an opening below the machine, ensuring cleanliness and hygiene in the processing area. In the egg sorting process, advanced sorting systems equipped with various sensors meticulously detect quality parameters such as weight, color, shape, and cracks. Operators can easily inspect eggs using a tubular lamp while handling the infeed and packing, ensuring that only eggs meeting specific quality standards are selected.
This technology is TAAT1 validated.
| Project | Countries | Beneficiaries | Budget (USD) & duration | Key figures |
|---|---|---|---|---|
|
ENSURE Enabling Environments for Sustainable Regional Agriculture Extension |
|
|
13.14 million 2024–2027 |
|
Figures in italic are from project plans and may change during implementation.
Adults 18 and over: Positive high
The poor: No impact
Under 18: Positive medium
Women: Positive high
Farmer climate change readiness: Significant improvement
Carbon footprint: A bit less carbon released
Environmental health: Moderately improves environmental health
Water use: A bit less water used
Mechanized defeathering and egg sorting technology improves poultry processing efficiency, food safety, product quality, and market access by reducing labor requirements, processing time, and product losses. It can be integrated into poultry value chain development, agribusiness promotion, women’s economic empowerment, youth employment, and food safety programs. Its adoption contributes to SDG 1 (No Poverty), SDG 2 (Zero Hunger), SDG 5 (Gender Equality), and SDG 8 (Decent Work and Economic Growth).
To integrate this technology into your project, plan and budget for the following activities and prerequisites:
Egg sorting machine
Unknown
Scaling Readiness describes how complete a technology's development is and its ability to be scaled. It produces a score that measures a technology's readiness along two axes: the level of maturity of the idea itself, and the level to which the technology has been used so far.
Each axis goes from 0 to 9 where 9 is the “ready-to-scale” status. For each technology profile in the e-catalogs we have documented the scaling readiness status from evidence given by the technology providers. The e-catalogs only showcase technologies for which the scaling readiness score is at least 8 for maturity of the idea and 7 for the level of use.
The graph below represents visually the scaling readiness status for this technology, you can see the label of each level by hovering your mouse cursor on the number.
Read more about scaling readiness ›
Uncontrolled environment: tested
Common use by intended users, in the real world
| Maturity of the idea | Level of use | |||||||||
| 9 | ||||||||||
| 8 | ||||||||||
| 7 | ||||||||||
| 6 | ||||||||||
| 5 | ||||||||||
| 4 | ||||||||||
| 3 | ||||||||||
| 2 | ||||||||||
| 1 | ||||||||||
| 1 | 2 | 3 | 4 | 5 | 6 | 7 | 8 | 9 | ||
| Project | Countries | Beneficiaries | Budget (USD) & duration | Key figures |
|---|---|---|---|---|
|
ENSURE Enabling Environments for Sustainable Regional Agriculture Extension |
|
|
13.14 million 2024–2027 |
|
Figures in italic are from project plans and may change during implementation.
| Country | Testing ongoing | Tested | Adopted |
|---|---|---|---|
| Benin | –No ongoing testing | –Not tested | Adopted |
| Botswana | –No ongoing testing | –Not tested | Adopted |
| Burundi | –No ongoing testing | –Not tested | Adopted |
| Central African Republic | –No ongoing testing | –Not tested | Adopted |
| Côte d'Ivoire | –No ongoing testing | –Not tested | Adopted |
| Ethiopia | –No ongoing testing | –Not tested | Adopted |
| Gabon | –No ongoing testing | –Not tested | Adopted |
| Ghana | –No ongoing testing | –Not tested | Adopted |
| Kenya | –No ongoing testing | –Not tested | Adopted |
| Madagascar | –No ongoing testing | –Not tested | Adopted |
| Malawi | –No ongoing testing | –Not tested | Adopted |
| Mozambique | –No ongoing testing | –Not tested | Adopted |
| Niger | –No ongoing testing | –Not tested | Adopted |
| Nigeria | –No ongoing testing | –Not tested | Adopted |
| Rwanda | –No ongoing testing | –Not tested | Adopted |
| Senegal | –No ongoing testing | –Not tested | Adopted |
| Sierra Leone | –No ongoing testing | –Not tested | Adopted |
| Somalia | –No ongoing testing | –Not tested | Adopted |
| South Sudan | –No ongoing testing | –Not tested | Adopted |
| Tanzania, United Republic | –No ongoing testing | –Not tested | Adopted |
| The Democratic Republic of the Congo | –No ongoing testing | –Not tested | Adopted |
| Uganda | –No ongoing testing | –Not tested | Adopted |
| Zambia | –No ongoing testing | –Not tested | Adopted |
| Zimbabwe | –No ongoing testing | –Not tested | Adopted |
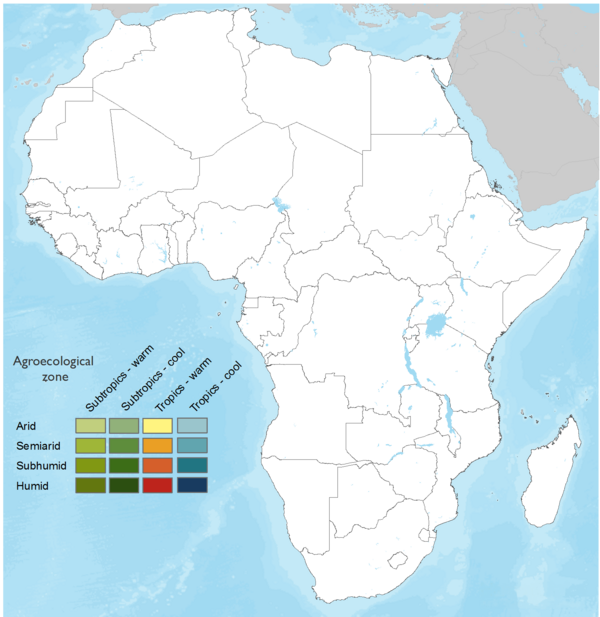
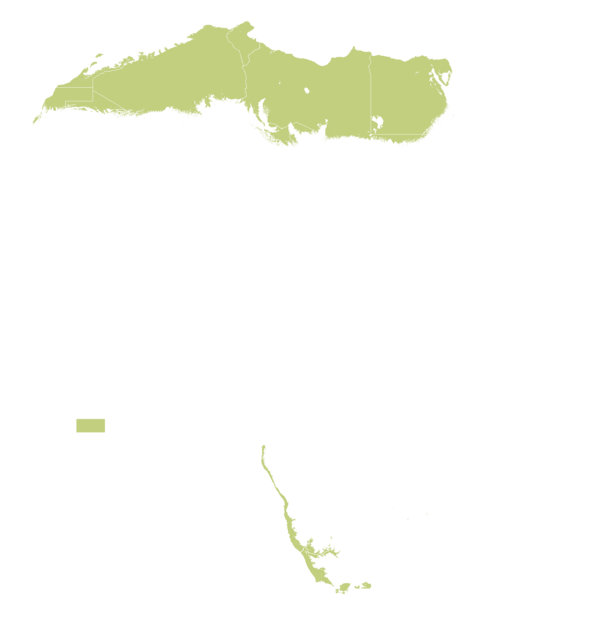
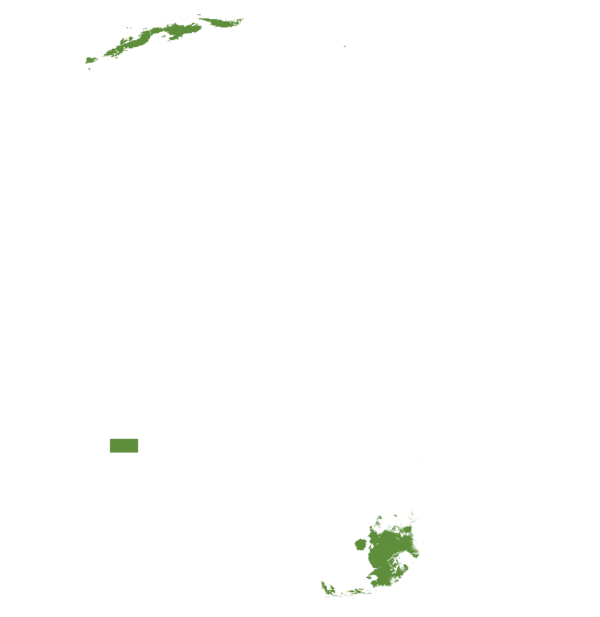
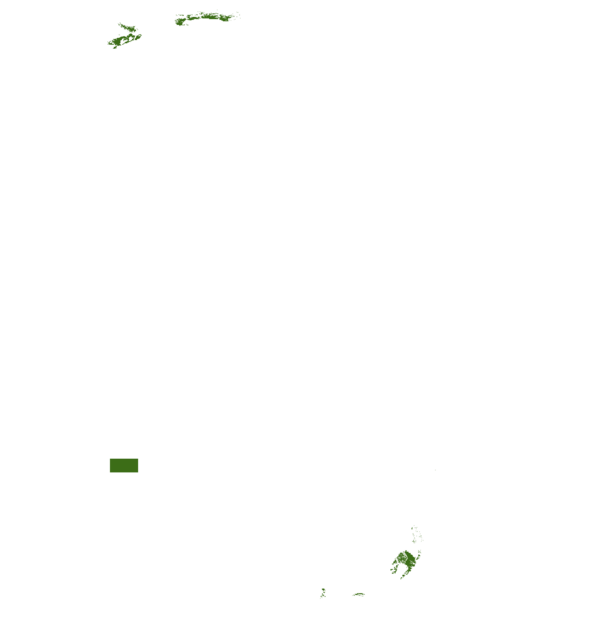
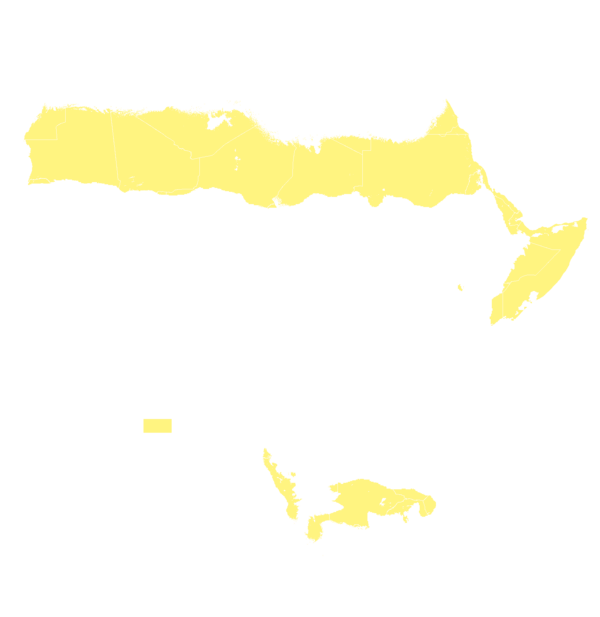
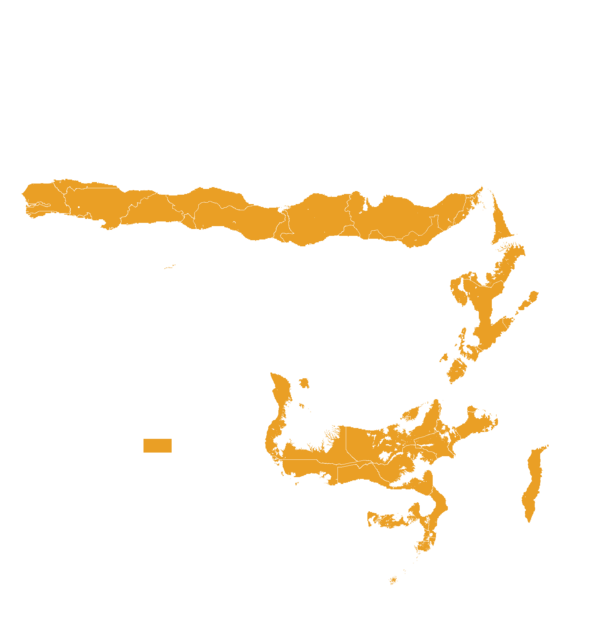
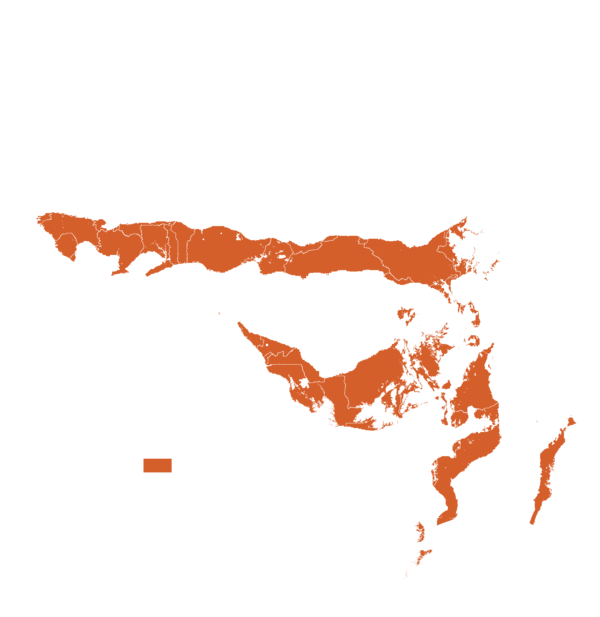
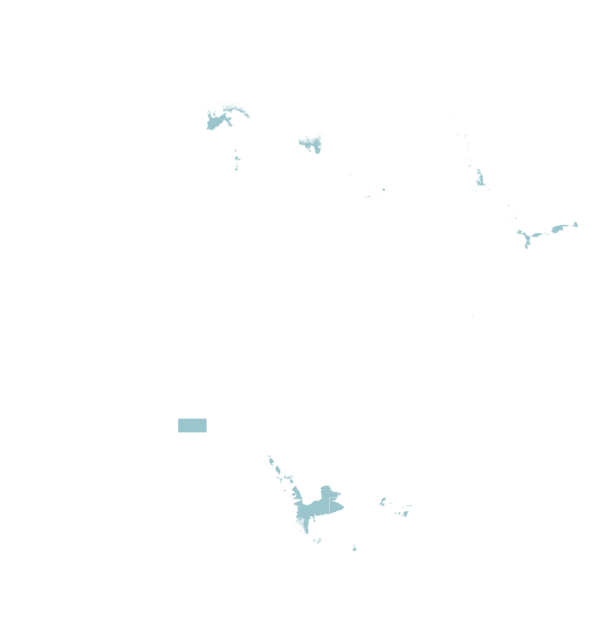
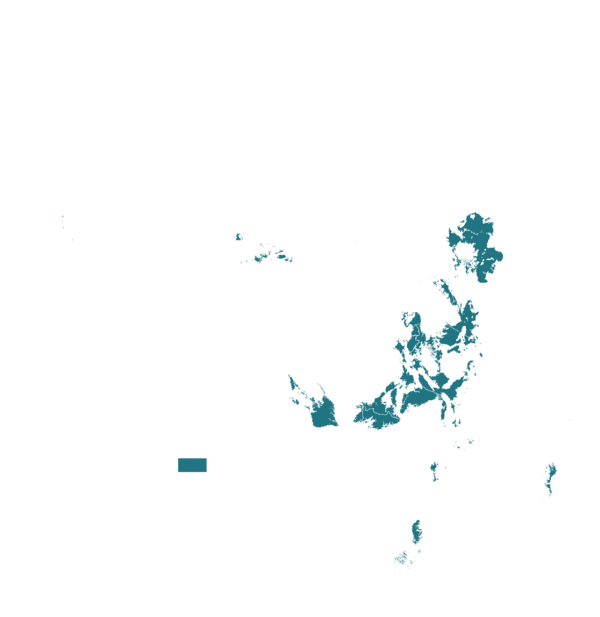
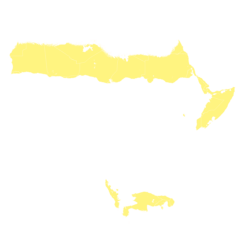
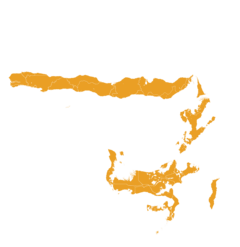
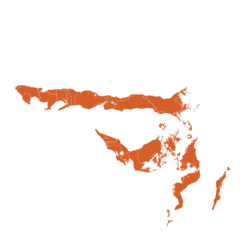
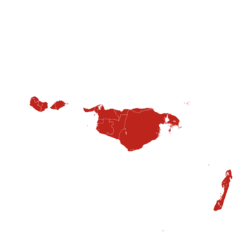
This technology can be used in the colored agro-ecological zones. Any zones shown in white are not suitable for this technology.




| AEZ | Subtropic - warm | Subtropic - cool | Tropic - warm | Tropic - cool |
|---|---|---|---|---|
| Arid | ||||
| Semiarid | ||||
| Subhumid | ||||
| Humid |
Source: HarvestChoice/IFPRI 2009
The United Nations Sustainable Development Goals that are applicable to this technology.
Defeathering Process:
Egg Sorting Process:
General Requirements:
Post-Processing:
Last updated on Oct 1, 2026
This technology can be used in the colored agro-ecological zones.






Mechanized Defeathering and Egg Sorting
https://e-catalogs.taat-africa.org/org/technologies/mechanized-defeathering-and-egg-sorting
Last updated on 1 October 2026, printed on Oct 23, 2026
Enquiries e-catalogs@taat.africa